






Precision Manufacturing, Connected

From eyewear components to precision parts, supporting development, sampling and volume production.

12Product CategoriesOEMDrawing & Sample BasedQCProcess Quality Control

Est. 2005 | Full-Chain Manufacturing & In-House Testing

To Be Your Reliable Partner

JYD Optitech Company Limited is a leading vertically integrated manufacturer in the global eyewear industry. Our head office is located in Longgang District, Shenzhen — the core area of China's mid-to-high-end eyewear manufacturing. We firmly believe that product quality and on-time delivery are the cornerstones of our business. All operations and development of our company are centered around these core priorities. Since 2005, the company has invested more than RMB 30 million, steadily deepening its expertise across every stage of a wide range of eyewear accessories.

Our Production Capabilities

With 20+ years of continuous investment and development, we have built a complete eyewear industrial chain. Our product range includes:

Stampings, Castings, Etched Parts, Injection Molded Parts, Hinges, Rim-locks, Wire rims. Based on our self-sufficient production of core components without reliance on external suppliers, our full-chain manufacturing system guarantees stable quality, controllable lead times and cost advantages for all our partners.

JYD Workshop1/1

Products & Services

See Our Factory

Tech & Tips

Micro Vickers Hardness Testing for the Eyewear Industry

Micro-indentation data supports material selection, process validation and quality decisions.

The Complementarity of Video Measuring Machines and Digital Projectors in the Eyewear Industry

The previous two articles introduced video measuring machines and digital projectors respectively, including their basic functions, principles, practical applications in the eyewear industry, and their respective advantages. No one is perfect, and the moon waxes and wanes; the same goes for measuring instruments. Only by complementing each other's strengths can they safeguard eyewear quality.

Wide Application of Video Measuring Machines in Eyewear Production

The previous article introduced the digital projector. When more precise measurement data is required, a Video Measuring Machine is needed.

Application of Digital Measuring Projectors in Eyewear Production

Eyewear parts are small and varied in shape, and in the past they were mostly judged with magnifying glasses and measuring tools. Digital measuring projectors magnify and project the outline of a part onto a screen, making edges, shapes and positional relationships more intuitive.

Spring Hinge 20,000-Cycle Durability Test Record

I. Test Background and Purpose

A Tool for Twisting

In the eyewear industry, temple shapes, decorations, patterns, and designs are incredibly diverse, and manufacturing techniques vary from maker to maker. This article focuses on one such technique, with emphasis on its production process and the tools used.

The Lost-Wax Casting Process for Metal Eyewear Components

Lost-wax casting is well suited to metal parts with complex shapes, fine details, or both decorative and structural functions. In production, wax is first formed into wax patterns matching the shape of the target part. The patterns are then assembled into a wax tree, and plaster slurry is poured around it to form the casting mold. After dewaxing by burnout, a cavity remains inside the mold; molten metal is then poured in, and after cooling, a cast blank is obtained.

Effect and Analysis of Extrusion Processing on Material Hardness

In the processing of eyewear metal components, hydraulic forming causes plastic deformation of the material, and hardness may change accordingly. This article uses a cupronickel product as an example to compare hardness records before the first hydraulic pressing, after the first hydraulic pressing, and after a second pressing and edge trimming. The test force for this test was 500 gf, and the average was taken after 5 measurements; the instrument type, measurement point locations at each stage, and raw readings still need to be verified.

Contact Us

Reach us by email or find our address and contact information.

ken@jyd-optitech.com
Tech & Tips

Effect and Analysis of Extrusion Processing on Material Hardness

In the processing of eyewear metal components, hydraulic forming causes plastic deformation of the material, and hardness may change accordingly. This article uses a cupronickel product as an example to compare hardness records before the first hydraulic pressing, after the first hydraulic pressing, and after a second pressing and edge trimming. The test force for this test was 500 gf, and the average was taken after 5 measurements; the instrument type, measurement point locations at each stage, and raw readings still need to be verified.

Before the first hydraulic pressing, the average hardness measured on the cylindrical cupronickel material after wire drawing was HV141.39 (Figure 1). This value falls within the half-hard 1/2H range (HV130–160) used in the article. Figure 1 only shows the material appearance; the hardness value before wire drawing was not included in this record; the above range also needs to be confirmed based on the specific material grade and product standard.

Article image 1
Article image 1

Figure 1 Appearance of cylindrical cupronickel material

After the first hydraulic pressing, the average hardness of the workpiece was HV215.56, an increase of 74.17 HV compared with before hydraulic pressing. The hardness increase of this part is consistent with the phenomenon of cold work hardening. The appearance of the workpiece after the first hydraulic pressing is shown in Figure 2.

After the second pressing and edge trimming, the average hardness was HV215.07, a decrease of 0.49 HV compared with after the first hydraulic pressing. The average values after both processings are within the 190–220 HV range used in the article; the correspondence between this range and the SH grade needs to be confirmed in conjunction with material standards. Due to the lack of readings for each measurement point and information on measurement fluctuation, the effect of the second processing on hardness cannot be judged solely based on the 0.49 HV difference. The appearance of the secondary processed part is shown in Figure 3.
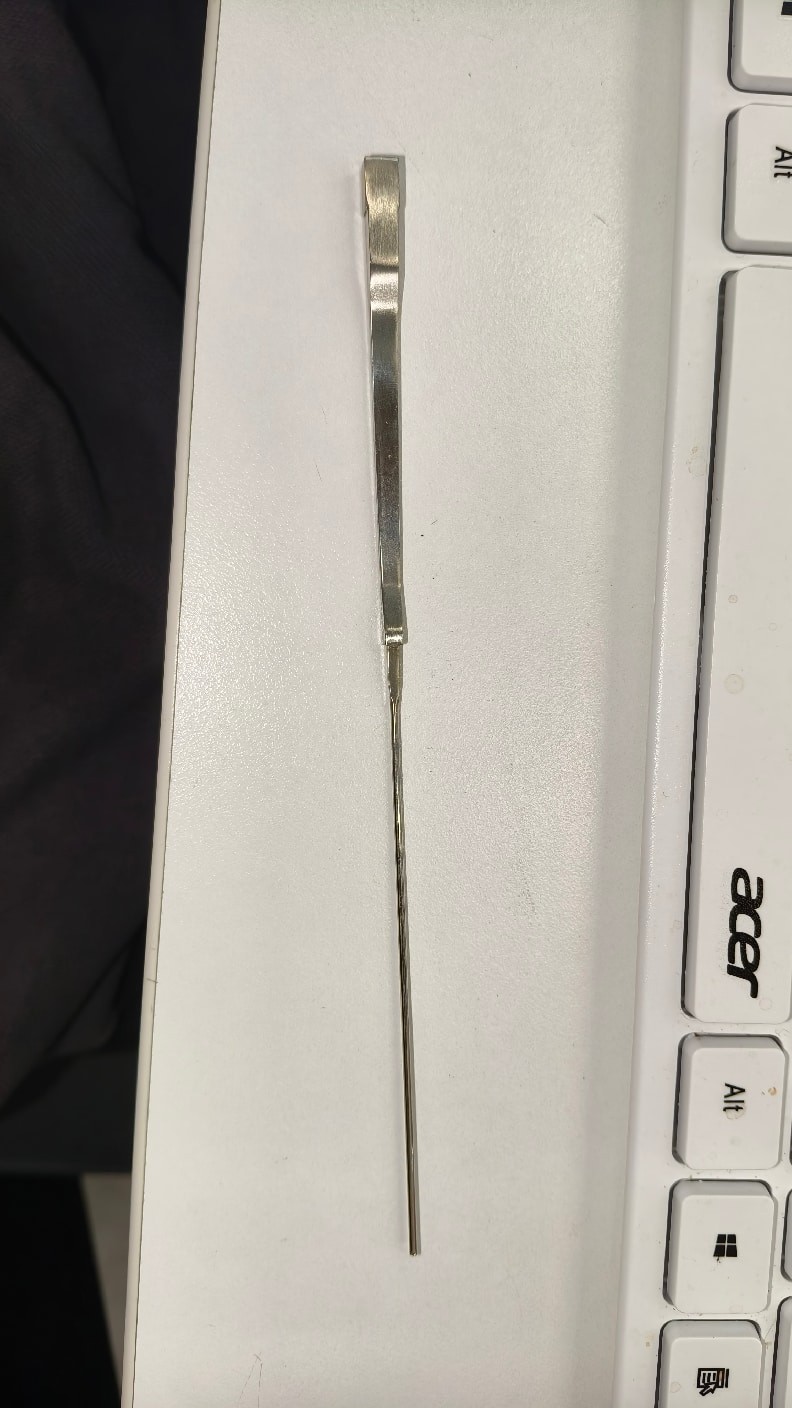
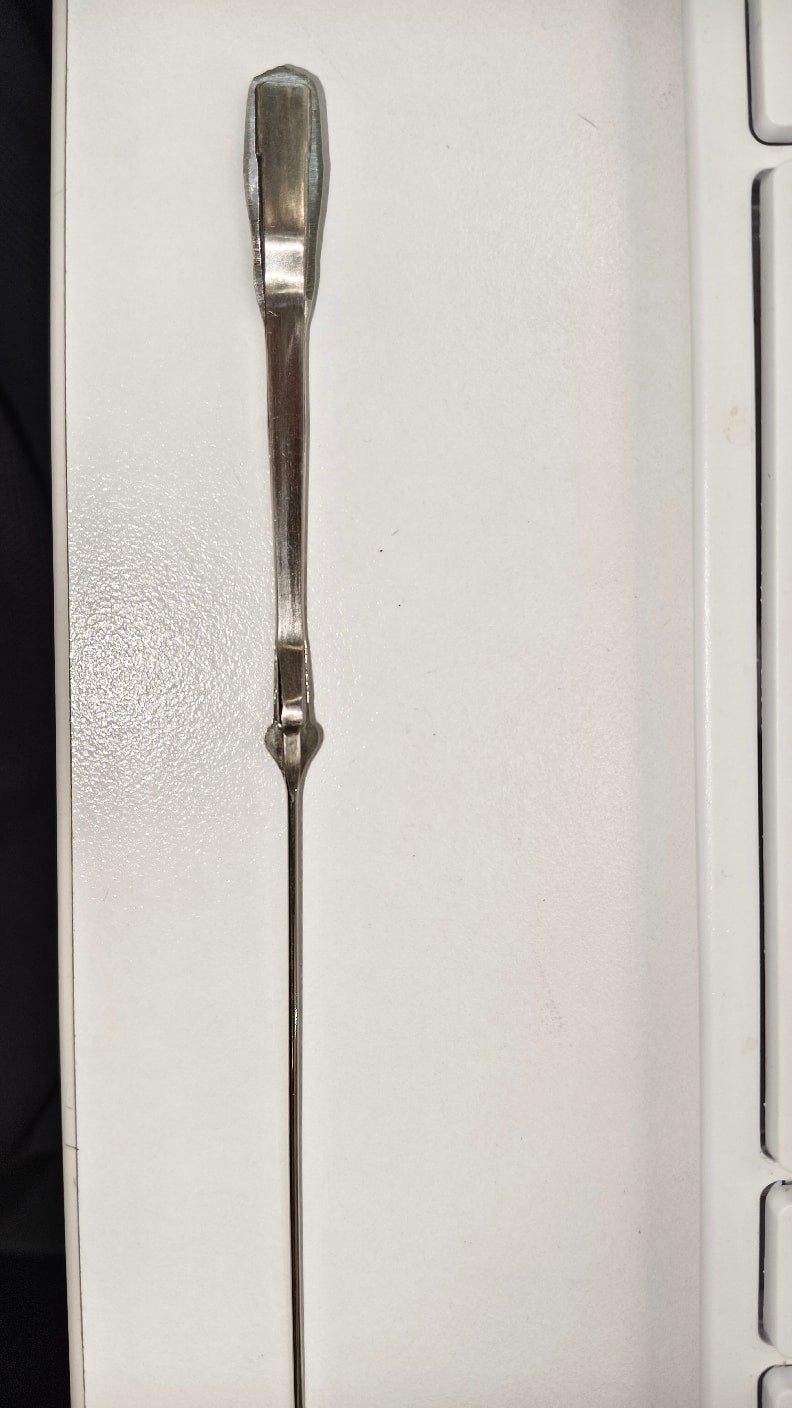
Article image 2
Article image 2
Article image 3
Article image 3

Figure 2 (left) Workpiece after the first hydraulic pressing Figure 3 (right) Appearance of the secondary processed part

For this part, the hardness after the first hydraulic pressing was higher than before hydraulic pressing, and the average value after the second edge trimming was close to the value after the first hydraulic pressing. Since the actual deformation amount and measurement point data are not listed, this record cannot infer a general relationship between deformation amount and hardness change. For microscopic Vickers hardness testing, please refer to article 004 "Application of Microscopic Vickers Hardness Testing in Eyewear Manufacturing"; the testing method actually used in this article still needs to be confirmed based on instrument records. If you would like to learn more or supplement on-site data, please contact us. Thank you for reading.

Contact Us